- +91 7302256783
- cohibapharma@gmail.com

Pharmaceutical Product Quality Control: How Medicines Are Tested Before Reaching the Market
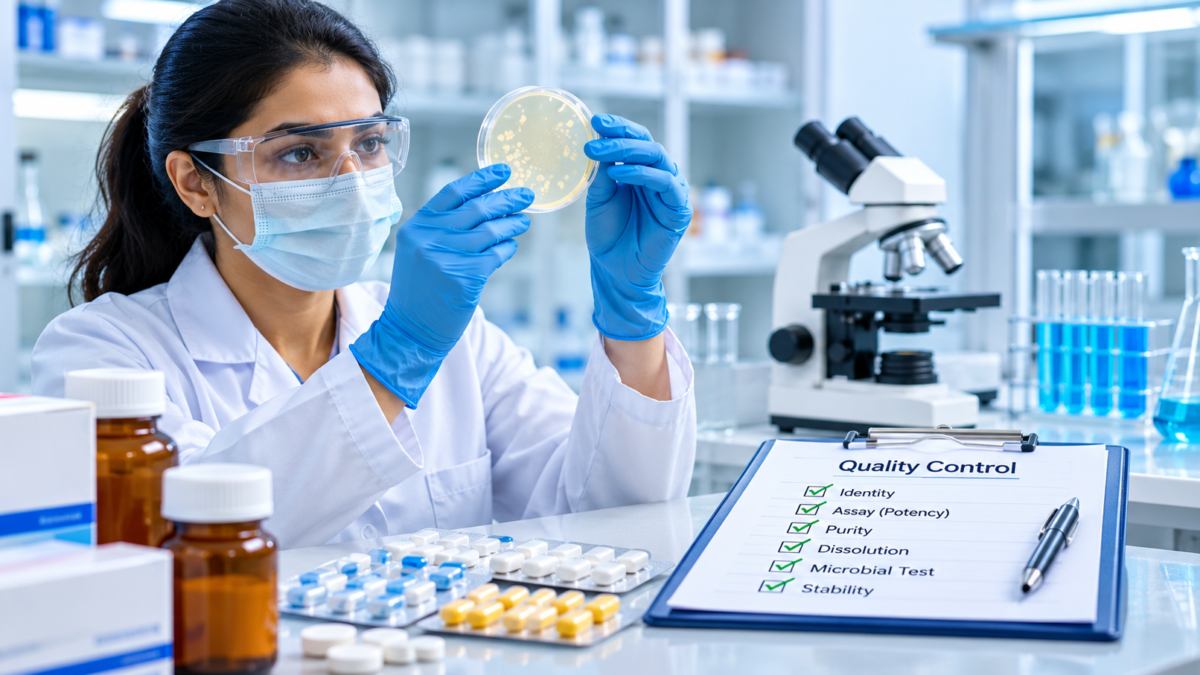
Pharmaceutical product quality control is one of the most important processes in the pharmaceutical industry. Every medicine must meet defined quality standards to ensure that it is suitable for its intended use, consistent in composition and manufactured under controlled conditions. From raw material inspection to final product testing, quality control helps identify defects and maintain the reliability of pharmaceutical products.
Medicines pass through several stages of manufacturing, testing, packaging and documentation before they are released for distribution. These processes help pharmaceutical companies maintain product consistency and comply with applicable regulatory requirements.
Understanding how pharmaceutical quality control works is essential for manufacturers, distributors, stockists and other professionals involved in the pharmaceutical supply chain.
What Is Pharmaceutical Product Quality Control?
Pharmaceutical product quality control refers to the systematic testing and inspection of raw materials, in-process materials and finished medicines to confirm that they meet established quality specifications.
It involves laboratory testing, physical inspections, documentation and other checks performed at different stages of pharmaceutical manufacturing.
The main purpose is to verify that a product meets its approved specifications for characteristics such as:
- Identity and composition
- Strength and concentration
- Purity and impurity levels
- Physical appearance
- Dissolution or disintegration, where applicable
- Microbiological quality, where required
- Stability throughout its specified shelf life
Quality control is closely connected to quality assurance. While quality control focuses on testing and verifying products, quality assurance covers the broader systems and procedures designed to prevent quality problems.
Why Is Quality Control Important in the Pharmaceutical Industry?
The quality of pharmaceutical products directly affects patient safety and the reliability of healthcare services. Inconsistent ingredients, contamination, incorrect strength or unsuitable storage conditions can compromise product quality.
An effective quality control system helps pharmaceutical companies maintain consistent manufacturing standards and identify potential issues before products are released.
1. Helps Maintain Product Consistency
Medicines manufactured in different batches should meet the same approved specifications. Quality control testing helps verify that each batch maintains the required composition, strength and quality characteristics.
2. Supports Patient Safety
Testing helps identify problems such as contamination, incorrect ingredient quantities and unacceptable impurities. This reduces the risk of unsuitable products entering the supply chain.
3. Helps Meet Regulatory Requirements
Pharmaceutical companies must follow applicable manufacturing and quality requirements. Proper testing, documentation and quality systems help demonstrate that products are manufactured and evaluated under controlled conditions.
4. Improves Manufacturing Processes
Quality testing can reveal recurring issues during production. Companies can investigate the causes, implement corrective measures and improve their manufacturing processes.
5. Builds Confidence Among Healthcare Professionals
Consistent product quality is important for doctors, pharmacists, distributors and other healthcare professionals. A reliable quality management system supports confidence in pharmaceutical products and the companies supplying them.
Key Stages of Pharmaceutical Product Quality Control
Quality control is not limited to testing the finished medicine. It begins with the materials used in manufacturing and continues through production, packaging and product release.
1. Raw Material Testing
The first stage involves checking the raw materials received from suppliers. These may include active pharmaceutical ingredients (APIs), excipients and other materials required for manufacturing.
Testing and inspection may include:
- Verification of material identity
- Assessment of purity and quality
- Physical and chemical testing
- Review of supplier documentation
- Checking material specifications and storage conditions
Materials should be approved according to established procedures before they are used in production.
2. In-Process Quality Checks
During manufacturing, quality checks are performed at different production stages. These checks help identify variations before they affect the finished product.
Depending on the dosage form and manufacturing process, in-process checks may include:
- Weight variation
- Tablet hardness and thickness
- Granule moisture content
- Mixing uniformity
- Fill volume
- pH measurement
- Appearance and physical consistency
The applicable tests depend on the product specifications and manufacturing requirements.
3. Finished Product Testing
Once manufacturing is completed, the finished product undergoes testing to confirm that it meets the required specifications.
Common tests may include:
Identification testing: Confirms the presence of the intended active pharmaceutical ingredient.
Assay testing: Measures the amount or concentration of the active ingredient in the product.
Dissolution testing: Evaluates how a drug is released from certain dosage forms under specified laboratory conditions.
Disintegration testing: Checks how quickly tablets or capsules break down under defined test conditions.
Uniformity testing: Evaluates whether individual dosage units contain consistent amounts of the active ingredient.
Microbiological testing: Assesses microbial quality where applicable, including tests for specified microorganisms or sterility for products that require it.
Not every test applies to every medicine. The testing programme is determined by the product type, approved specifications and relevant pharmacopoeial or regulatory requirements.
4. Packaging and Labelling Inspection
Packaging plays an important role in protecting pharmaceutical products from environmental exposure, contamination and physical damage.
Quality checks may include:
- Verification of product name and strength
- Batch number and manufacturing details
- Manufacturing and expiry dates
- Packaging integrity
- Seal and closure inspection
- Label accuracy and readability
- Storage instructions and other required information
Incorrect labelling or damaged packaging can create serious problems during storage, distribution and use. Therefore, packaging checks are an important part of the quality control process.
5. Stability Testing
Stability testing evaluates how the quality of a pharmaceutical product changes over time under specified environmental conditions.
It helps establish or support the product’s shelf life and recommended storage conditions.
Depending on the product and applicable guidelines, stability studies may assess:
- Temperature-related changes
- Humidity effects
- Physical appearance
- Chemical degradation
- Active ingredient concentration
- Packaging compatibility
- Microbiological quality, where relevant
Stability data helps determine whether a medicine continues to meet its specifications during its intended storage period.
Quality Control Tests for Different Pharmaceutical Dosage Forms
Different pharmaceutical products require different testing procedures because their physical properties, ingredients and intended routes of administration vary.
| Dosage form | Examples of quality checks |
| Tablets | Weight variation, hardness, friability, disintegration and dissolution |
| Capsules | Weight variation, content uniformity and dissolution |
| Syrups | Appearance, pH, assay and microbial quality |
| Dry syrups | Moisture content, reconstitution characteristics and stability |
| Injectables | Sterility, bacterial endotoxins where applicable, particulate matter and assay |
| Suspensions | Particle characteristics, redispersibility, pH and assay |
| Topical gels | Appearance, pH, viscosity and assay |
| Oral drops | Assay, fill volume, appearance and microbial quality where applicable |
The exact tests and acceptance criteria must be based on the relevant product specifications and applicable standards.
Role of Good Manufacturing Practices (GMP) in Quality Control
Good Manufacturing Practices (GMP) provide a framework for maintaining quality throughout pharmaceutical manufacturing. They cover the systems, procedures, facilities, equipment and personnel involved in producing medicines.
GMP supports quality control by establishing requirements for:
- Qualified and trained personnel
- Suitable manufacturing facilities
- Equipment maintenance and calibration
- Approved raw material suppliers
- Documented manufacturing procedures
- Batch manufacturing and testing records
- Hygiene and contamination prevention
- Deviation investigation and corrective actions
- Proper storage and distribution practices
Quality control testing and GMP work together. Testing checks whether a product meets its specifications, while GMP helps ensure that the processes used to manufacture it are properly controlled.
Importance of Documentation and Batch Records
Documentation is a fundamental part of pharmaceutical quality management. It provides evidence that materials, manufacturing activities, inspections and testing have been completed according to approved procedures.
Important records may include:
- Raw material test reports
- Certificates of Analysis (CoA)
- Batch Manufacturing Records
- Batch Packaging Records
- In-process testing reports
- Finished product test reports
- Stability study records
- Equipment calibration records
- Deviation and corrective action reports
Batch records also support traceability. If a quality issue is identified, documented information helps the company investigate the affected batch and take appropriate action.
How Pharmaceutical Companies Can Maintain Consistent Product Quality
Maintaining quality requires a planned approach rather than relying on final product testing alone. Pharmaceutical companies should establish effective quality management systems and review them regularly.
Some important practices include:
Working with qualified suppliers: Raw materials should be sourced from evaluated suppliers and checked according to approved procedures.
Maintaining controlled manufacturing conditions: Equipment, facilities and production processes should be suitable for the products being manufactured.
Following approved testing procedures: Laboratory tests should use validated or otherwise appropriately qualified methods, as required.
Training employees: Personnel involved in manufacturing, testing, packaging and storage should receive relevant training.
Maintaining proper storage conditions: Pharmaceutical products and raw materials should be stored according to their specified conditions.
Investigating quality deviations: Unexpected results and manufacturing deviations should be documented, investigated and addressed through appropriate corrective and preventive actions.
These practices help support product consistency and strengthen quality management across the pharmaceutical supply chain.
Choosing a Pharmaceutical Company: Why Quality Standards Matter
When selecting a pharmaceutical company for a business partnership, distributors and pharma franchise professionals should consider more than product availability and commercial terms. Quality systems, documentation and regulatory compliance are also important factors.
Before entering into a partnership, it is useful to review:
- Relevant manufacturing and marketing authorisations
- Applicable GMP-related documentation
- Product specifications and Certificates of Analysis, where available
- Batch traceability and quality documentation
- Product storage and distribution arrangements
- Procedures for handling complaints and quality-related concerns
Documents and certifications should be checked for authenticity, validity and applicability to the specific products and manufacturing facilities involved.
Cohiba Pharmaceuticals: A Focus on Pharmaceutical Product Quality
Cohiba Pharmaceuticals Pvt. Ltd., based in Dehradun, Uttarakhand, operates in the pharmaceutical sector and offers a range of pharmaceutical product categories and PCD pharma franchise opportunities.
For distributors and prospective business partners, understanding product specifications, relevant documentation, manufacturing arrangements and applicable quality requirements is an important part of evaluating any pharmaceutical company.
Conclusion
Pharmaceutical product quality control is essential for maintaining the safety, consistency and reliability of medicines. It involves multiple stages, including raw material inspection, in-process checks, finished product testing, packaging inspection and stability studies.
An effective quality control system, supported by Good Manufacturing Practices, trained personnel and accurate documentation, helps pharmaceutical companies maintain defined product standards and meet applicable regulatory requirements.
For manufacturers, distributors and pharma franchise professionals, understanding these processes makes it easier to evaluate pharmaceutical products and build responsible business relationships. Quality should remain a priority throughout the pharmaceutical supply chain, from manufacturing to final distribution.
Frequently Asked Questions (FAQs)
1. What is pharmaceutical product quality control?
Pharmaceutical product quality control is the process of testing and inspecting raw materials, products during manufacturing and finished medicines to confirm that they meet established quality specifications.
2. What are the main stages of pharmaceutical quality control?
The main stages include raw material testing, in-process quality checks, finished product testing, packaging and labelling inspection, and stability testing.
3. What is the difference between quality control and quality assurance in pharma?
Quality control focuses on testing and verifying materials and products against defined specifications. Quality assurance covers the wider systems and procedures designed to ensure that quality is consistently maintained.
4. Why is GMP important in pharmaceutical manufacturing?
Good Manufacturing Practices help ensure that medicines are consistently produced and controlled according to appropriate quality standards. They cover manufacturing processes, personnel, facilities, equipment and documentation.
5. How can distributors evaluate the quality of pharmaceutical products?
Distributors can review relevant product documentation, manufacturing and marketing authorisations, applicable GMP records, Certificates of Analysis, batch details and storage requirements. They should verify that the documents are authentic and relevant to the products being supplied.